Anti-UV Polyester Dope Dyed Filament Yarn Company: The Future of Durable and Eco-Conscious Textiles
2026-08-06
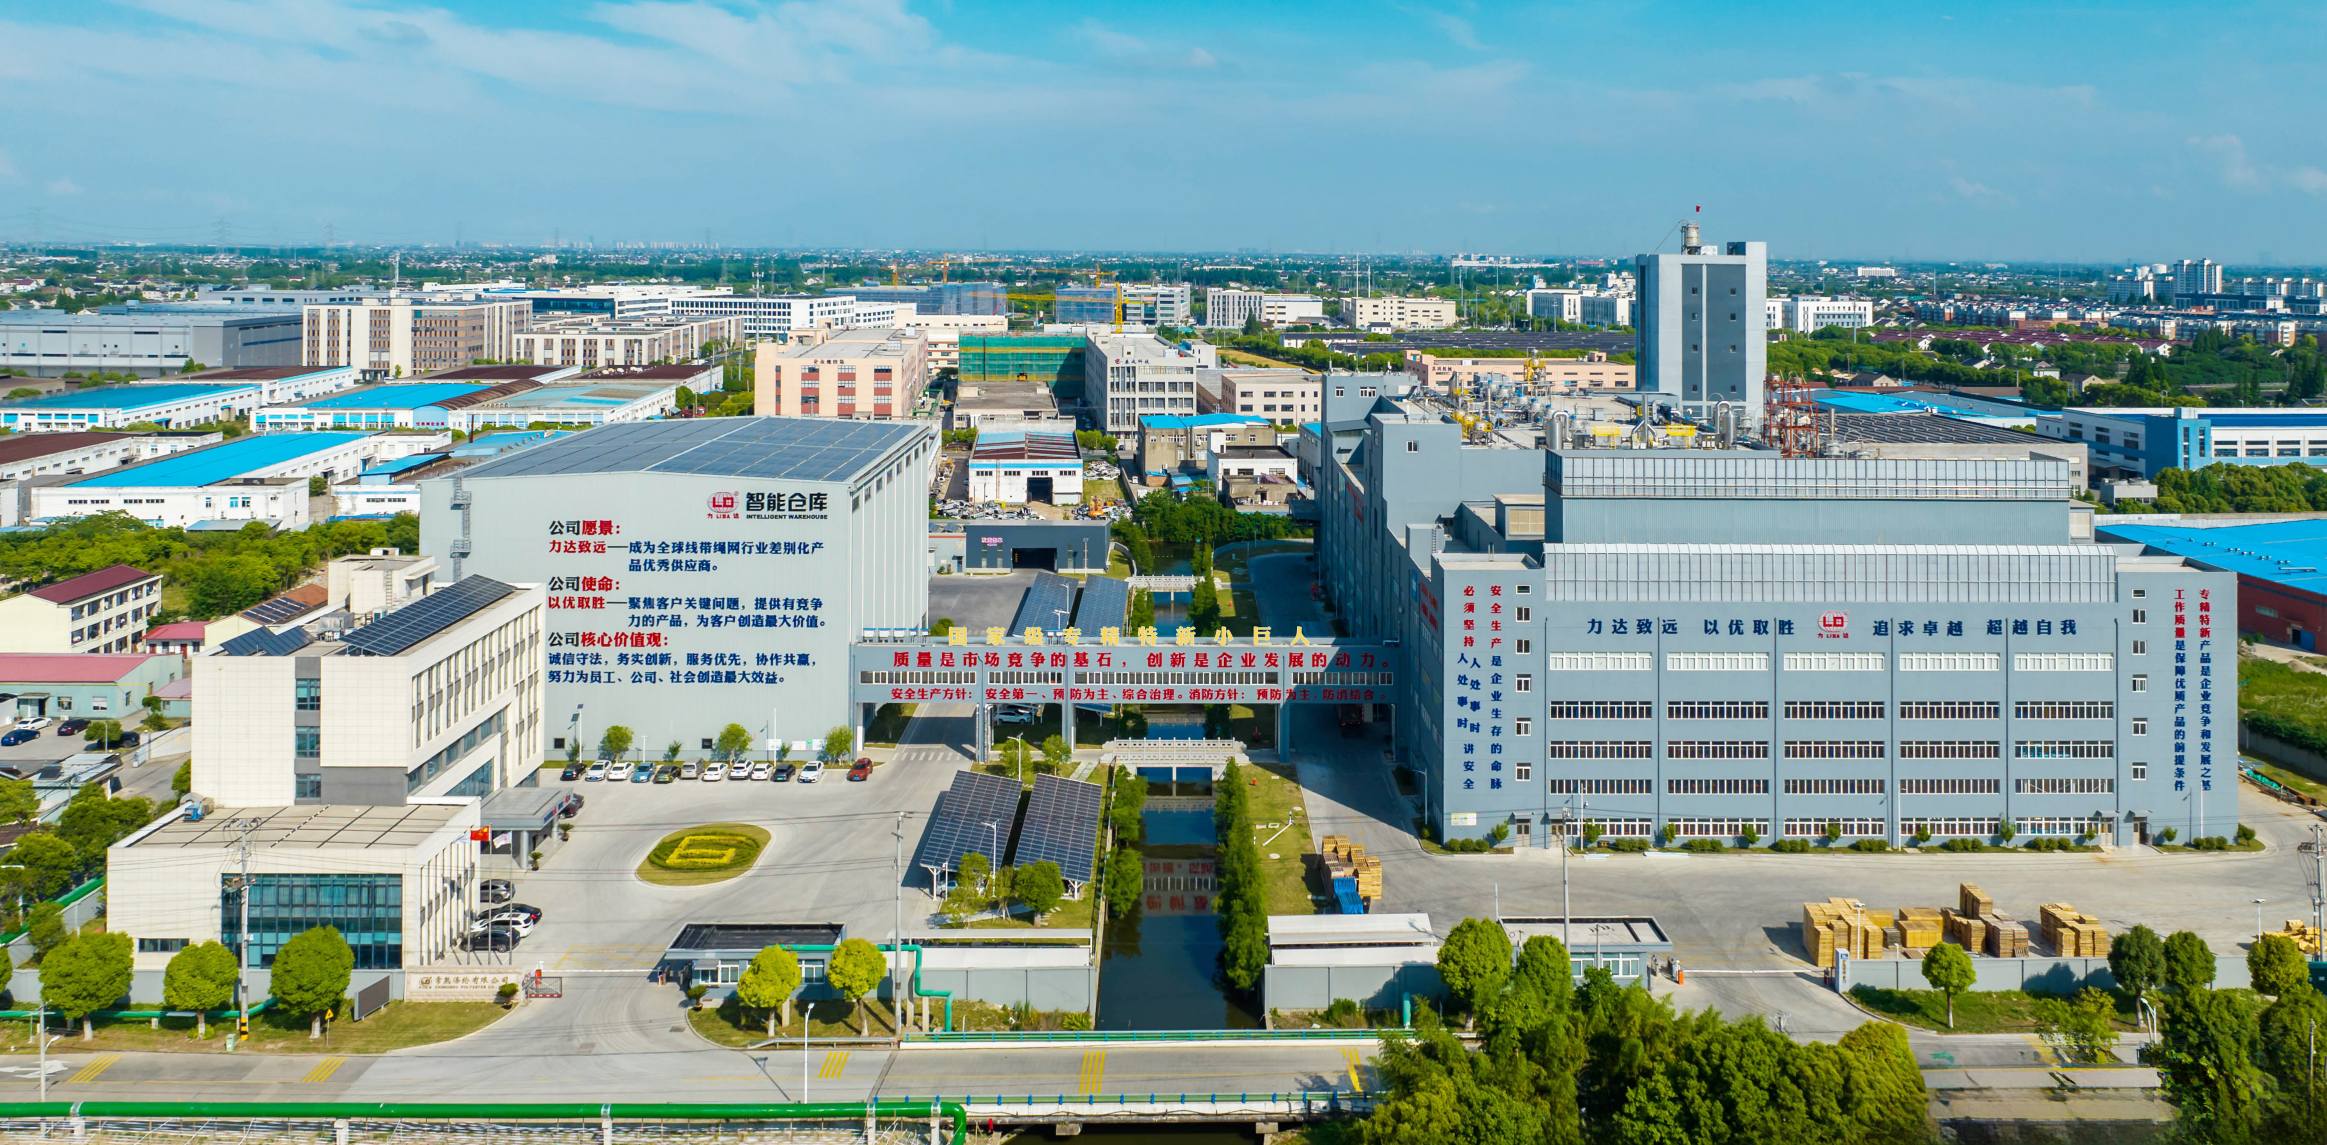
When durability meets sustainability, something transformative happens in textiles. Anti-UV polyester dope dyed filament yarn is quietly reshaping how we think about long-lasting, eco-aware fabrics—and Changshu Polyester is at the heart of this shift. Behind every thread lies a smarter, greener approach to everything from outdoor gear to everyday fashion.
Innovations in UV-Resistant Yarn Production
Recent breakthroughs in polymer chemistry have paved the way for yarns that inherently block harmful ultraviolet rays without compromising flexibility or colorfastness. By integrating nano-scale titanium dioxide particles directly into the spinning solution, manufacturers can now produce fibers with UV protection woven into their core. This method ensures that the resistance doesn’t wash off or degrade over time, addressing a long-standing weakness of topical treatments. The result is a softer, more durable yarn suitable for everything from outdoor apparel to architectural textiles.
Another significant stride is the development of bio-based UV absorbers derived from lignin and other plant extracts. These natural compounds are chemically bound to the polymer chains during extrusion, offering an eco-friendly alternative to synthetic additives. Beyond shielding from sunlight, they introduce subtle antioxidant properties that slow down fiber aging. Early adopters in the sportswear sector are already blending these yarns into lightweight, high-UPF garments that maintain breathability and comfort even after extended exposure.
On the machinery side, advanced false-twist texturing now allows precise control over yarn bulk and surface structure, enhancing UV scattering without extra coatings. By engineering crimp geometry and filament cross-sections, producers create yarns that physically deflect a broader spectrum of radiation. This mechanical approach complements chemical methods and opens up new possibilities for recyclable, mono-material fabrics with inherent sun protection—eliminating the need for multi-layered fabrics and simplifying end-of-life processing.
Sustainable Practices in Dope Dyeing
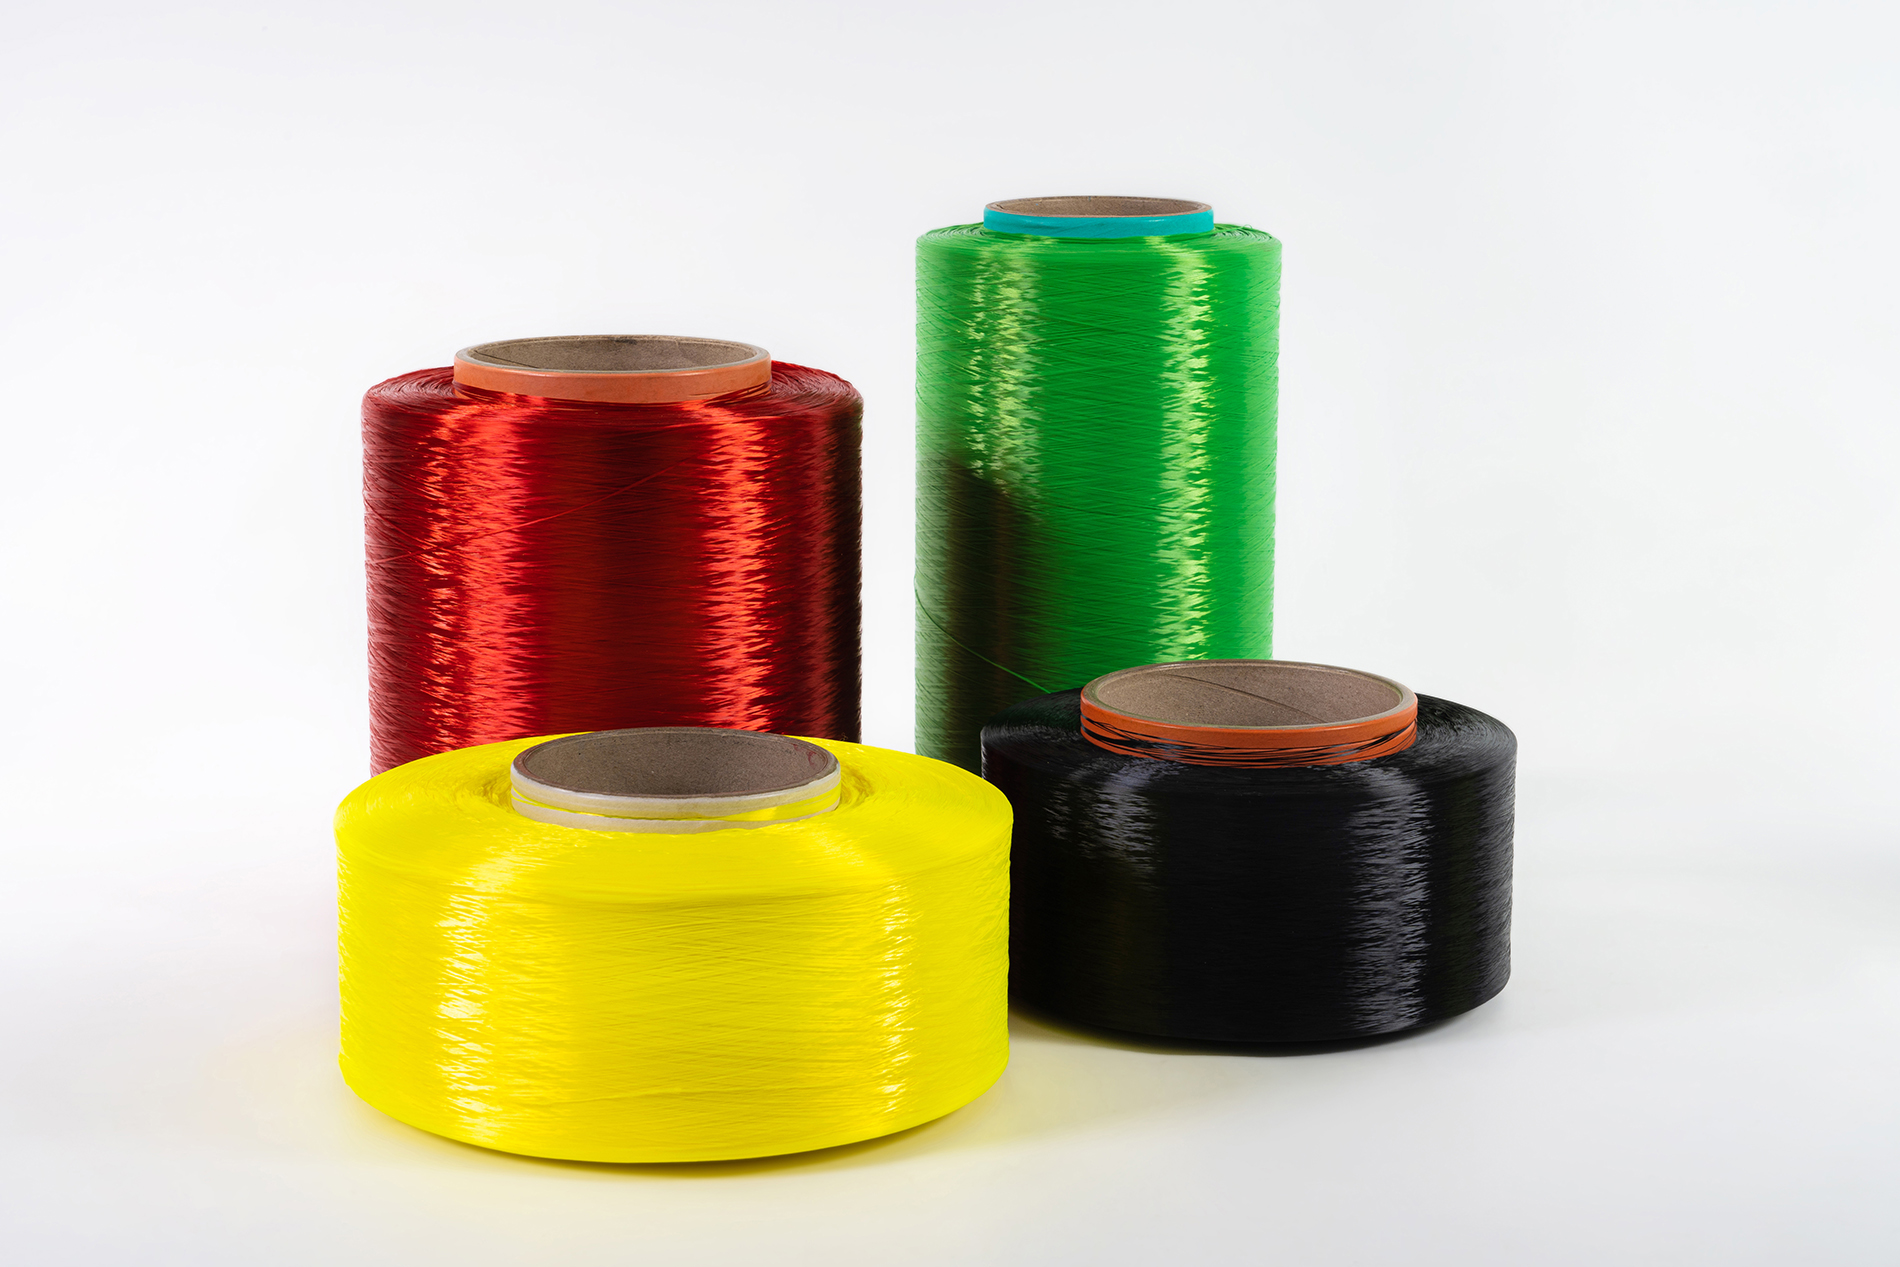
Dope dyeing, also known as solution dyeing, fundamentally reimagines textile production by infusing pigments directly into the polymer melt before fiber extrusion. This process eliminates the need for water-intensive post-spinning baths, a radical departure from conventional piece dyeing where countless liters are consumed to fix color onto fabric. The water savings are staggering—up to 90% reduction in some operations—while simultaneously cutting chemical usage, since auxiliaries like leveling agents and salts become unnecessary. What often goes unnoticed is the energy efficiency: skipping the drying phase post-dyeing shrinks a factory's carbon footprint substantially, making dope dyeing a quiet heavyweight in climate-conscious manufacturing.
Beyond resource conservation, dope dyeing delivers exceptional colorfastness that extends the functional life of textiles. By embedding pigment within the fiber's core rather than clinging to its surface, the color resists fading from light, abrasion, and repeated laundering. This longevity means garments maintain their aesthetic appeal far longer, subtly discouraging the wear-and-discard cycle that plagues fast fashion. Industrial applications are particularly telling—outdoor furniture, automotive interiors, and military gear rely on this technique to withstand harsh elements without bleeds or runs, proving that durability is itself a sustainability strategy.
The technique's compatibility with recycled synthetics opens a progressive frontier. Post-consumer PET bottles can be melted, blended with colorant, and spun into fresh polyester yarn without the quality degradation that often hampers mechanical recycling. This circular approach reduces dependency on virgin petrochemicals and diverts plastic waste from landfills, all while producing fabrics that require no further dyeing. As brands grapple with green transparency, dope dyeing offers verifiable metrics—every kilogram of fabric produced can be directly linked to specific resource savings, giving eco-conscious consumers tangible proof of impact rather than vague marketing.
Durability Meets Eco-Conscious Design
Durable design isn’t just about surviving wear and tear—it’s about creating pieces that age gracefully while respecting the planet. We’ve shifted from the throwaway mindset by using high-tenacity recycled fibers that outlast conventional materials, yet decompose responsibly at end of life. Every stitch and seam is reinforced, not merely to extend product lifespan, but to reduce the frequency of replacement and, in turn, waste.
Our obsession with longevity pairs naturally with a transparent supply chain. Instead of hiding behind vague claims, we detail exactly how each component is sourced—from reclaimed ocean plastics molded into resilient casings to plant-based dyes that don’t compromise colorfastness. This isn’t about compromise; it’s about proving that environmental consciousness can amplify toughness, not dilute it.
The result is an object that tells a story of continuous use rather than disposable novelty. Scratches become patina, not defects, and modular components allow for effortless repairs instead of landfill trips. By aligning ruggedness with resourcefulness, we’re redefining what it means to build for the long haul—because true durability honors both the user and the environment.
How Anti-UV Filaments Redefine Fabric Longevity
Traditional fabrics often surrender to the sun’s relentless assault, fading and weakening long before their time. Anti-UV filaments change this narrative entirely by weaving protection directly into the yarn. Unlike topical coatings that wash away or degrade, these advanced fibers embed UV-stabilizing compounds at a molecular level. This means every thread inherently deflects harmful rays, preserving color vibrancy and tensile strength from the inside out. It’s a fundamental shift from surface-level defense to built-in resilience, ensuring the material holds its own against years of exposure.
The real magic lies in how these filaments distribute protection evenly across the entire textile. Because the UV-blocking components are part of the polymer matrix, there are no weak spots where sunlight can sneak through. This uniform shield drastically slows the breakdown of fiber structure, preventing the brittleness and micro-tears that normally accumulate over time. Outdoor gear, awnings, and marine upholstery now last significantly longer, maintaining their integrity and appearance without the need for frequent replacements. The fabric essentially becomes its own guardian, shrugging off the cumulative damage that typically shortens fabric lifespan.
Crafting Colorfast Textiles with Less Water
The traditional dyeing process is notoriously thirsty, often requiring vast amounts of water to fix pigments onto fibers. But a quiet revolution is unfolding in textile mills that are pioneering low-water techniques. By rethinking the chemistry at the molecular level, these methods allow dyes to bond more directly and durably with fabrics, slashing water usage without compromising the vibrancy or longevity of the color. It’s a shift that treats every drop as precious, turning an age-old craft into a model of resource intelligence.
One approach gaining traction replaces water as the primary solvent, using supercritical carbon dioxide instead. In this pressurized system, the CO2 acts like a gas with the density of a liquid, carrying dye deep into the fibers and then recycling the solvent in a closed loop. The result is color that penetrates evenly and sets fast, resisting fading through wash after wash. Factories adopting this method have cut their water consumption by up to 90 percent for certain fabrics, while also eliminating the heated drying steps that can weaken threads and dull hues.
Even where full solvent replacement isn’t feasible, advances in pigment encapsulation are making a difference. Microscopic polymer shells are used to encase color particles, enabling them to adhere directly to textiles through a simple heat press with minimal moisture. This not only conserves water but also strengthens the fabric’s resistance to light and abrasion. The end user sees a garment that holds its saturation beautifully, while the production story behind it is one of deliberate, measurable reduction in environmental load—a true win for both aesthetics and ecology.
The Role of Polyester Yarn in a Circular Economy
Polyester yarn is often seen as just another material in the fashion industry, but its potential in a circular economy is worth a closer look. When we start treating polyester not as a single-use resource but as a material that can keep its value through multiple lifecycles, things get interesting. Chemical recycling technologies are now breaking down polyester back to its monomers, allowing it to be remade into new yarn without the quality loss you'd see in mechanical recycling. It's a process that doesn't just reduce waste; it rethinks waste as a starting point.
Of course, the real challenge lies in the collection and sorting infrastructure. Even the best recycling technology won't help if the polyester textiles don't make it back into the loop. That's where brands and municipalities need to step up, designing garments for disassembly and making take-back schemes as normal as trash collection. When these systems click, polyester yarn becomes a textbook example of circularity—moving from textile to yarn and back again, with minimal resource drain.
Then there's the design side. Using polyester yarn in a circular economy isn't just about recycling; it's about making products that are meant to be recycled from the start. Think monomaterial garments, easy-to-remove trims, and dyes that don't interfere with the chemical recycling process. When designers and manufacturers align their choices with the realities of end-of-life processing, polyester yarn transforms into a key player in a system where nothing is wasted, only reused.
FAQ
Unlike traditional yarns that rely on surface treatments for UV protection and color, this yarn integrates UV-blocking pigments directly into the polymer during the melt-spinning process. This results in a material where the protective and color properties run through the entire filament, offering vastly superior colorfastness, lasting UV resistance, and no risk of coating degradation over time.
Dope dyeing eliminates the water-intensive and chemical-heavy wet dyeing stage altogether. By adding color before extrusion, the process saves enormous amounts of water, energy, and avoids discharging dye-laden wastewater. It’s a fundamentally cleaner method that significantly reduces the carbon and environmental footprint of textile manufacturing compared to piece-dyed fabrics.
The UV protection is permanent because the anti-UV agents are part of the fiber matrix itself, not a surface coating. It doesn’t wash off, wear away, or diminish with repeated laundering or prolonged sun exposure. You can expect the same level of UV shielding throughout the entire lifecycle of the fabric.
Applications that demand durability under harsh conditions see the biggest benefits: outdoor furniture, awnings, automotive interiors, sports and swimwear, military gear, and architectural sun-shading fabrics. Any product that needs to withstand constant UV exposure, moisture, and heavy use without fading or weakening is a perfect fit.
Through meticulous masterbatch formulation and advanced color measurement systems. Every batch of colored polymer chips is spectro-photometrically checked against strict standards before spinning begins. In-line monitoring and final skein testing ensure that each run matches the target shade with delta E values typically below 1.0, guaranteeing uniformity for large-scale projects.
The focus is moving toward bio-based polyester bases, enhanced mechanical recyclability without quality loss, and smart functionalities like thermal regulation or self-cleaning surfaces—all while keeping the core dope-dyed, UV-resistant advantages. Integrating circular economy principles with high-performance polymer science is the next big leap.
Conclusion
In an era where textile performance and environmental responsibility are no longer mutually exclusive, the Anti-UV Polyester Dope Dyed Filament Yarn Company stands at the forefront of innovation. By integrating UV-resistant properties directly into the yarn's core through advanced filament technologies, the company eliminates the need for surface treatments that wear off over time. This intrinsic shielding not only blocks harmful ultraviolet radiation more effectively but also preserves the fabric's integrity wash after wash. Unlike conventional methods that rely on resource-intensive wet processing, their dope dyeing technique infuses color pigments during the melt extrusion stage, slashing water consumption by up to 90% and preventing dye-laden effluent from entering ecosystems. The result is a yarn that embodies both resilience and sustainability, setting a new benchmark for industries seeking to reduce their ecological footprint without compromising on performance.
The durability of these yarns redefines fabric longevity in practical terms: garments and outdoor textiles retain their color and structural strength far longer, resisting fading, weakening, and degradation even under relentless sun exposure. This inherent colorfastness means products can endure years of use and repeated laundering with minimal water and energy, aligning perfectly with circular economy principles. By designing for extended lifespans, the company facilitates a shift away from disposable fast fashion and toward a model where materials remain in use longer, eventually being recycled into new polyester fibers. The marriage of UV resistance and dope dyed production thus becomes a cornerstone of eco-conscious design—enabling textiles that protect both the wearer and the planet. With every spool, the Anti-UV Polyester Dope Dyed Filament Yarn Company proves that durability and ecological awareness can be woven into the very fabric of our future.
Contact Us
Contact Person: CONNIE
Email: [email protected]
Tel/WhatsApp: 86-0512-53671634
Website: https://www.lida-yarn.com/