China Laser Cutting Machine Buying Guide and Expert Tips
2026-09-24
You're not buying a laser cutter; you're buying weeks of production uptime and a partner's response time. The China market is flooded with machines that look identical on paper but diverge sharply in beam quality, gantry rigidity, and service support. This buying guide skips the brochure language and focuses on what actually matters: real cutting performance on your materials, hidden costs in installation and training, and how to verify a manufacturer's claims before payment. I've included hard-won expert tips from workshops that learned the expensive way—so you don't have to. If you're comparing HUNSONE against other Chinese manufacturers, the checkpoints below will help you separate a dependable production tool from a garage gamble.
What Your First Quote Won't Tell You
When you get that first quote, the easiest thing to miss is what isn't listed. Taxes, disposal fees, temporary permits, even equipment usage charges—these often hide in the fine print or only surface halfway through the job. The number on the page looks clean, but once work actually starts, the total has a way of creeping upward.
Another thing most people don't realize is that the lowest bid usually means someone is cutting corners somewhere else. Maybe the materials get downgraded, the timeline gets squeezed so crews rush, or any kind of follow-up service simply isn't part of the deal. The few hundred dollars you save up front often turns into the cost of redoing, repairing, or hiring someone new later.
Then there's the part rarely mentioned: a quote is based on ideal conditions. Is there hidden plumbing behind that wall? Are the floor joists underneath suffering from moisture? Nobody knows until things are opened up. Once the site reality differs from the estimate, added charges become almost inevitable—and by then you've lost most of your leverage to negotiate.
Why Two 1000W Machines Aren't the Same
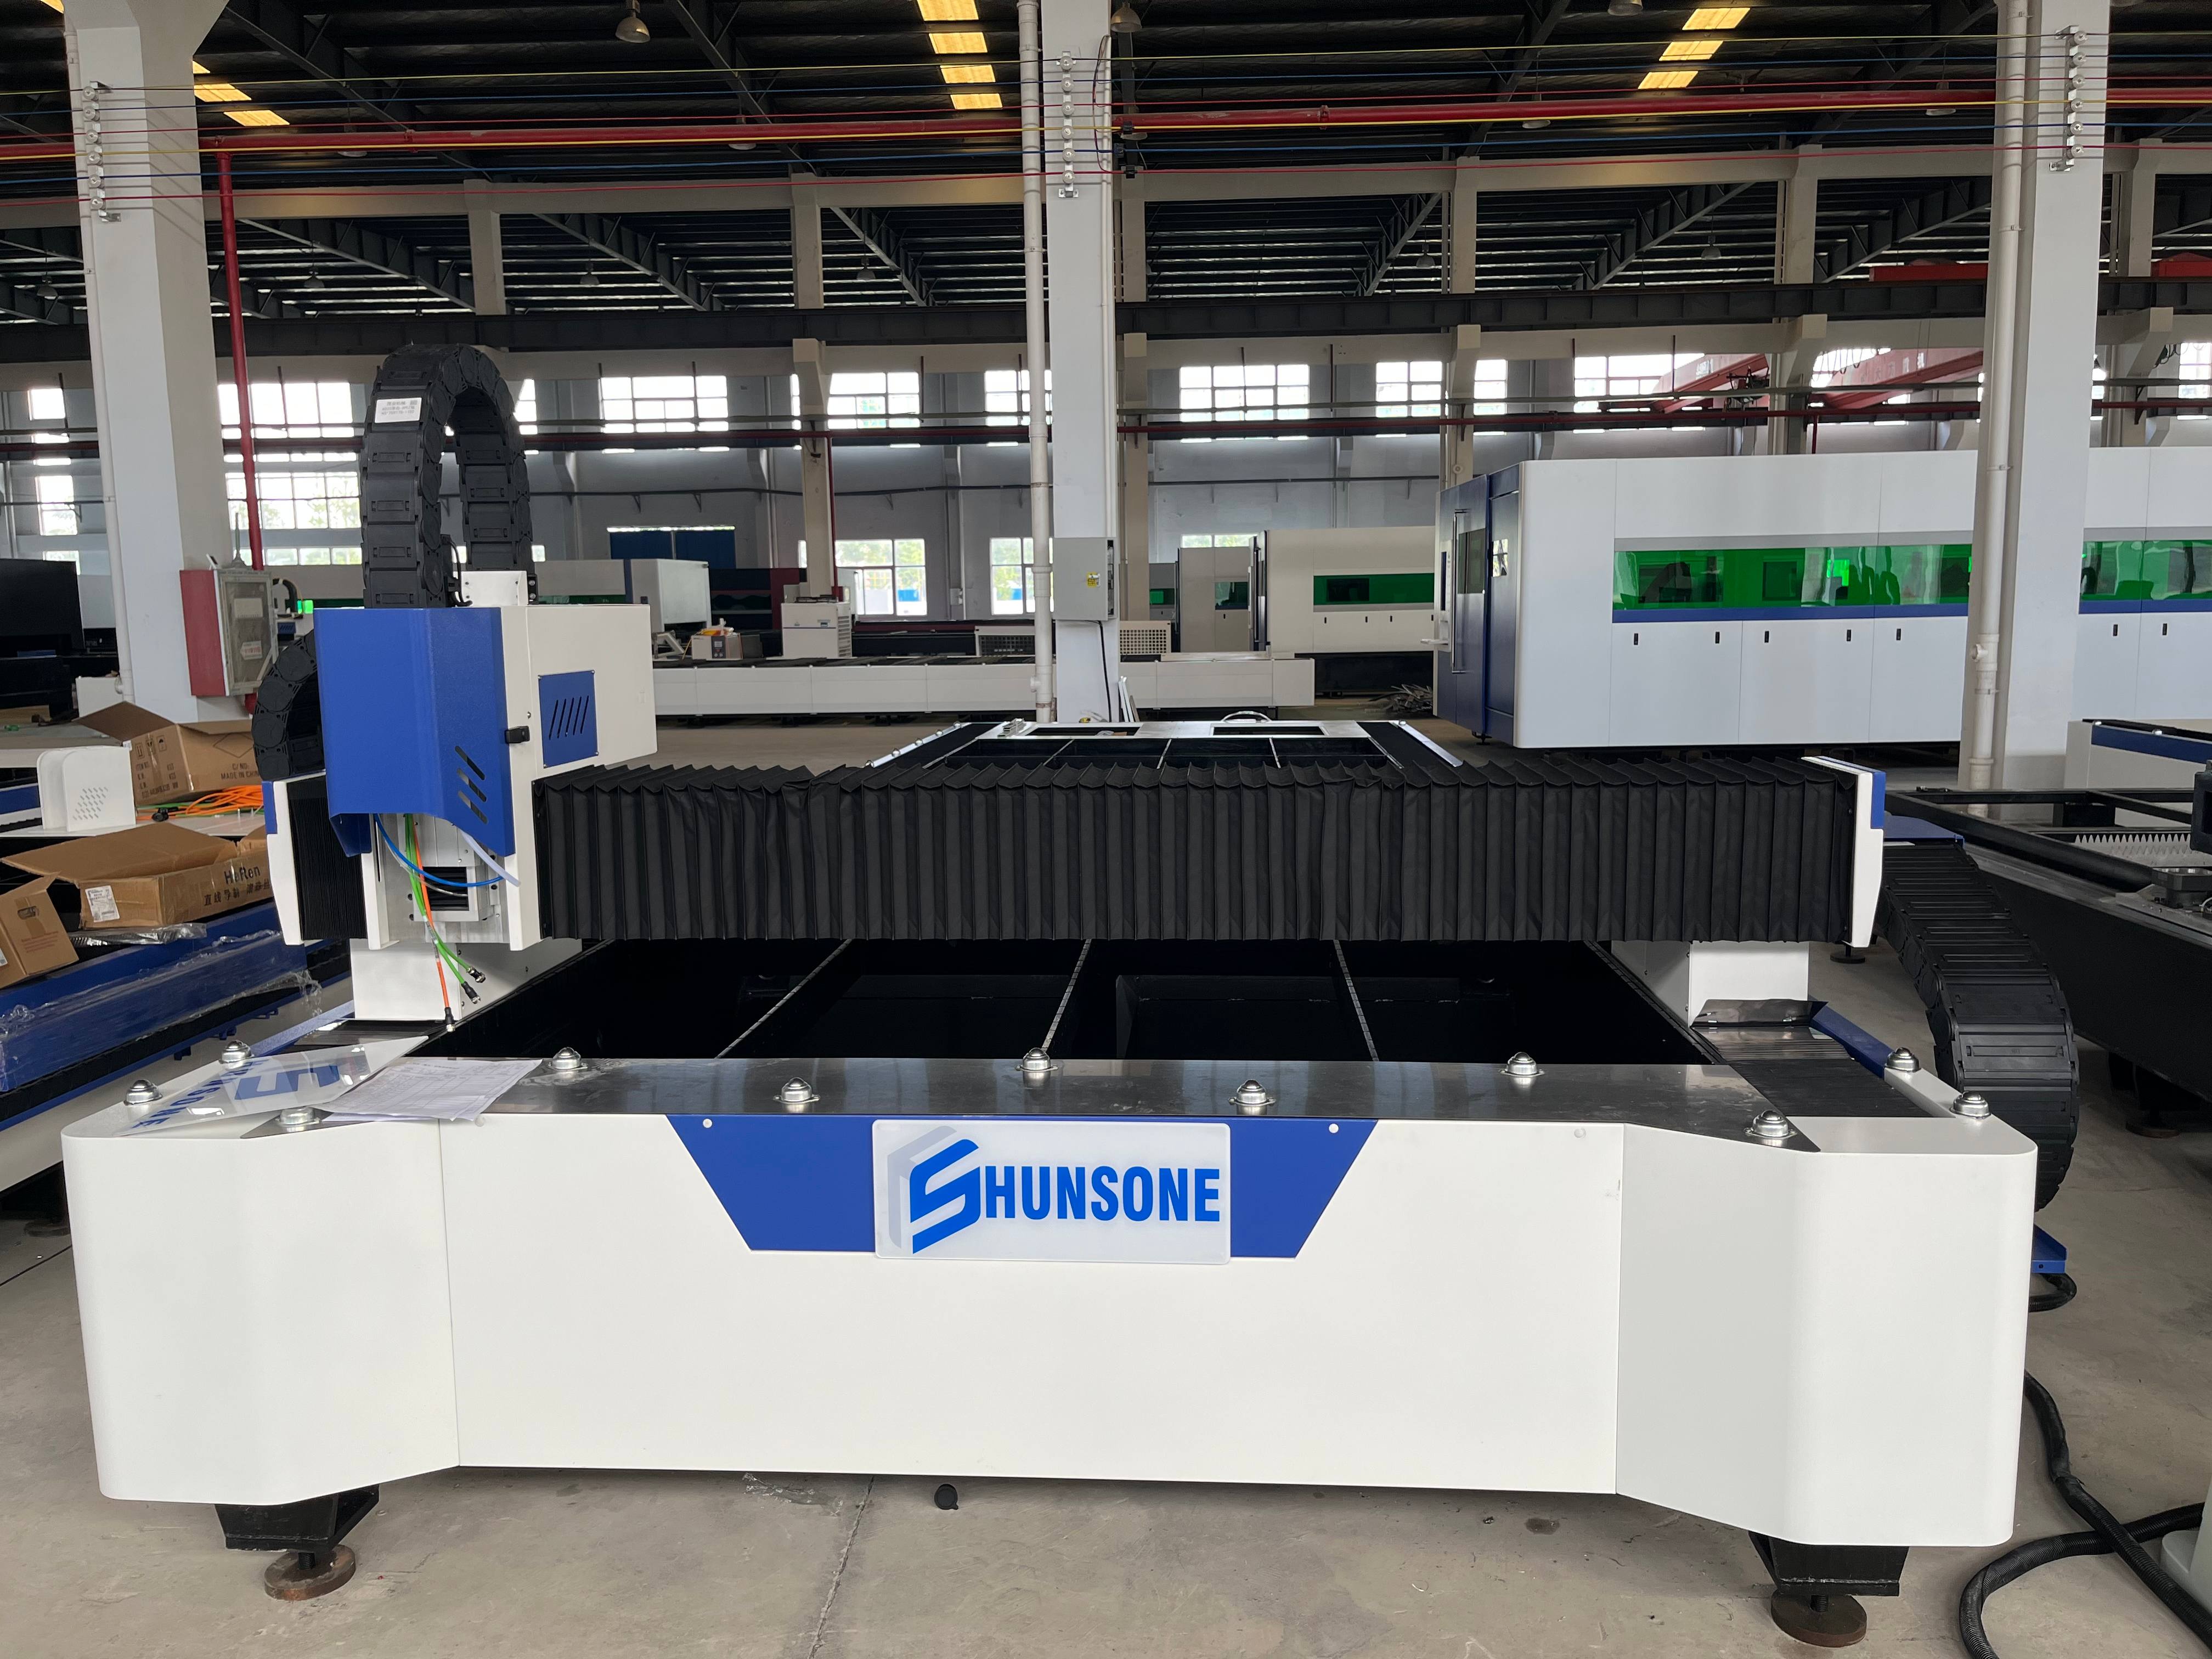
A wattage rating on paper rarely tells the whole story. One 1000W machine may deliver that figure as peak output for a few seconds before dropping, while another sustains close to that number continuously without overheating. The difference often comes down to how the motor is wound, the quality of the magnets, and the control electronics managing the power flow.
Cooling design, bearing tolerances, and even the power source can shift real-world performance. A brushed motor rated at 1000W will behave very differently from a brushless one under load, and a machine built with thinner internal wiring may lose more energy as heat. So two devices wearing the same number can feel nothing alike in actual use.
Factory Visits: What to Poke and Prod
When you walk onto a factory floor, don't just nod along with the tour guide. Look at how raw materials are stored—especially anything sensitive to moisture or heat. A pile of cardboard boxes sitting directly on concrete near a loading dock tells you more than any quality certificate. Ask to see the calibration stickers on measuring tools; if they're expired or scratched beyond reading, that's a red flag you can't ignore.
Another thing worth probing is the workflow between stations. Watch whether operators have to search for parts or walk long distances to fetch fixtures. If you spot a lot of improvised jigs or handwritten notes taped to machines, dig into why. These small patches often hint at deeper process instability. Also check the reject bins—not just the count, but the types of defects. A factory that openly shows you its scrap area and explains root causes is usually more trustworthy than one that hides it behind a curtain.
Maintenance logs are another goldmine. Flip through the last few pages rather than asking for a summary. Look for repeated entries like "replaced same bearing" or "adjusted sensor again." That pattern suggests chronic equipment issues that might delay your order later. Finally, pay attention to how workers react to your questions. If supervisors answer for them every time, or if the line stops just because you're standing there, you're not seeing normal production.
The Shipping Crate Is Half the Story
A crate rarely gets a second look once the lid is pried off, but the way it's built often reveals more than the item inside. The wood grain, the spacing of nails, the rough stenciling on one side—these details carry their own texture and timing. You can read a crate like a short letter if you know what to notice.
The weight shift when you tilt it, the sound of packing material shifting, even the faint smell of sawdust or salt from a long trip—none of that is accidental. Someone chose the thickness of the boards and the position of the handles for a reason. Those choices stay with you after the object is out and the crate is leaning against the garage wall.
Maybe that's why the crate itself lingers. It's not just protective casing; it's the first and last physical impression of a transaction. The object inside might be the reason for the shipment, but the crate is what you actually touch first, carry, and later decide to keep or break apart.
Bargaining in China Without Losing Face
In many Chinese markets, the first price quoted is rarely the final one, but pushing too hard can create tension. A better opening move is to ask for the "best price" in a friendly tone while showing genuine interest in the item. This signals that you are serious without immediately challenging the seller's position. If the initial quote remains high, pause, smile, and say something like "That's a bit more than I expected" rather than demanding a lower number outright.
Once the negotiation starts, use indirect language to suggest a lower amount. Instead of naming a price, ask if there is any flexibility or mention that you saw something similar for less elsewhere. This keeps the exchange from becoming a direct confrontation. If the seller drops the price even slightly, accept the movement gracefully with a nod or a small compliment, then continue from there. Saving face on both sides means neither you nor the seller should feel cornered into admitting defeat.
When you are close to a deal, avoid showing too much eagerness or triumph. A calm, almost reluctant agreement works better than celebrating a "win." If the final price is still above your target but reasonable, it is often wiser to accept it politely than to squeeze for the last few yuan and risk souring the interaction. In many cases, ending on good terms matters more than the exact amount saved, especially if you plan to return to the same stall or recommend it to others.
When the Support Line Goes Quiet
The first time the line went silent, it felt like a dropped call—an annoying glitch that would fix itself by the next attempt. You dialed again, expecting the familiar voice or the hold music, but got only the hollow click of an empty channel. Days passed, then weeks, and the silence stopped being a surprise. It became a presence, a quiet confirmation that whatever had been holding you up was no longer there.
Silence on a support line is rarely neutral. It asks questions you did not want to face: Was the help ever real, or just a performance? Did you lean too hard, exhaust the patience of someone who was only paid to listen? The absence of a response turns inward, and you start filling the quiet with your own doubts. That is when the real work begins—not fixing the problem you called about, but learning to sit with not being answered.
Yet quiet can also be an unexpected teacher. When no one picks up, you stop rehearsing what you would say and start hearing what you have been avoiding. The support line going silent does not mean you are abandoned; it means the script has ended. Whatever comes next will not be handed to you in a reassuring tone. It will be your own voice, unsteady at first, learning to be enough.
FAQ
Look beyond the price tag. Verify how long the factory has actually been manufacturing machines, ask for a live video tour of the production floor, and request references from buyers in your own country who purchased a similar wattage. A supplier with consistent assembly practices and clear documentation is far more valuable than the one offering the lowest quote.
It depends on the materials you cut most. Fiber lasers handle steel, aluminum, copper, and brass efficiently, need less maintenance, and have lower running costs. CO2 lasers still make sense for thicker non-metal work like wood, acrylic, leather, and some plastics. If your daily work is mostly sheet metal under 20mm, fiber is usually the smarter long-term choice.
A rough working guide: 1000W to 1500W covers up to 8mm mild steel and 4mm stainless with decent speed. 3000W handles 12mm mild, 6mm stainless, and 4mm aluminum comfortably. 6000W and above is for production shops cutting 20mm mild steel or 12mm stainless daily. Don't overbuy wattage unless your order volume justifies it—higher power means higher initial cost and more expensive replacement parts.
The machine may arrive with a generic controller or unlicensed software that limits future upgrades. Some factories substitute cheaper laser sources or cutting heads than the ones listed in the quote. Also, wiring and grounding issues can cause erratic behavior once connected to your local power supply. Always demand a detailed BOM, brand names for key components, and a factory acceptance test video before shipping.
It is often the deciding factor between a profitable machine and an expensive paperweight. Check if they offer remote diagnosis, how fast they ship replacement parts, and whether they have local service partners or a time zone overlap that works for you. Ask them to demonstrate remote software updates on a current customer's machine, not just promise it in the contract.
Request a live cutting test on your exact material thickness and grade, not just a demo on thin mild steel. Confirm the laser source brand, cutting head brand, chiller, and control system match the signed specification sheet. Have them run the machine for at least 30 minutes continuously while you watch via video. If possible, hire a third-party inspection company in China to check the crate and packaging before loading.
For most buyers, a standard proven configuration is safer. Customization often means the factory is building something for the first time, which raises the risk of delays, wiring mistakes, and software conflicts. If you truly need a special bed size or automation feature, ask for at least two existing customer references with that exact custom setup before committing.
Beyond the machine price, plan for about 10-20% of the machine cost for shipping, port fees, import duties, and local taxes depending on your country. Installation and training might cost another $1,500 to $4,000 if the factory sends an engineer, or you can handle it yourself with good remote guidance. Always get a DDP or at least CIF quote so you know which costs are included.
Conclusion
Most buyers fixate on laser wattage and cutting speed from the first quote, but that sheet rarely reveals the hidden costs: chiller quality, lens lifespan, software licensing, and after-sales support. Two machines both labeled 1000W can differ wildly—one may use an unbranded fiber source and lightweight gantry, while another pairs a reliable IPG or Raycus source with a heat-treated bed and precision rails. These details determine whether your machine holds tolerance after 5,000 hours or drifts into rework. Savvy buyers ask for the bill of materials, not just the spec sheet, because that's where corners hide.
A factory visit tells you more than any datasheet. Check weld consistency on the frame, cable routing inside the cabinet, and whether the test cut matches your material—not just demo steel. The shipping crate is equally critical: weak bracing or missing moisture protection turns a perfect machine into a bent rail and rusted electronics by the time it reaches your port. When bargaining, avoid aggressive haggling over price alone; instead ask for upgraded components or spare parts, which maintains face and yields real value. Finally, clarify support expectations upfront—who answers when the line goes quiet, whether remote diagnostics exist, and how quickly replacement parts ship. Many hidden costs live in that silence.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/