Professional Press Brake Machine: Key Features and Applications for Precision Metalworking
2026-09-16
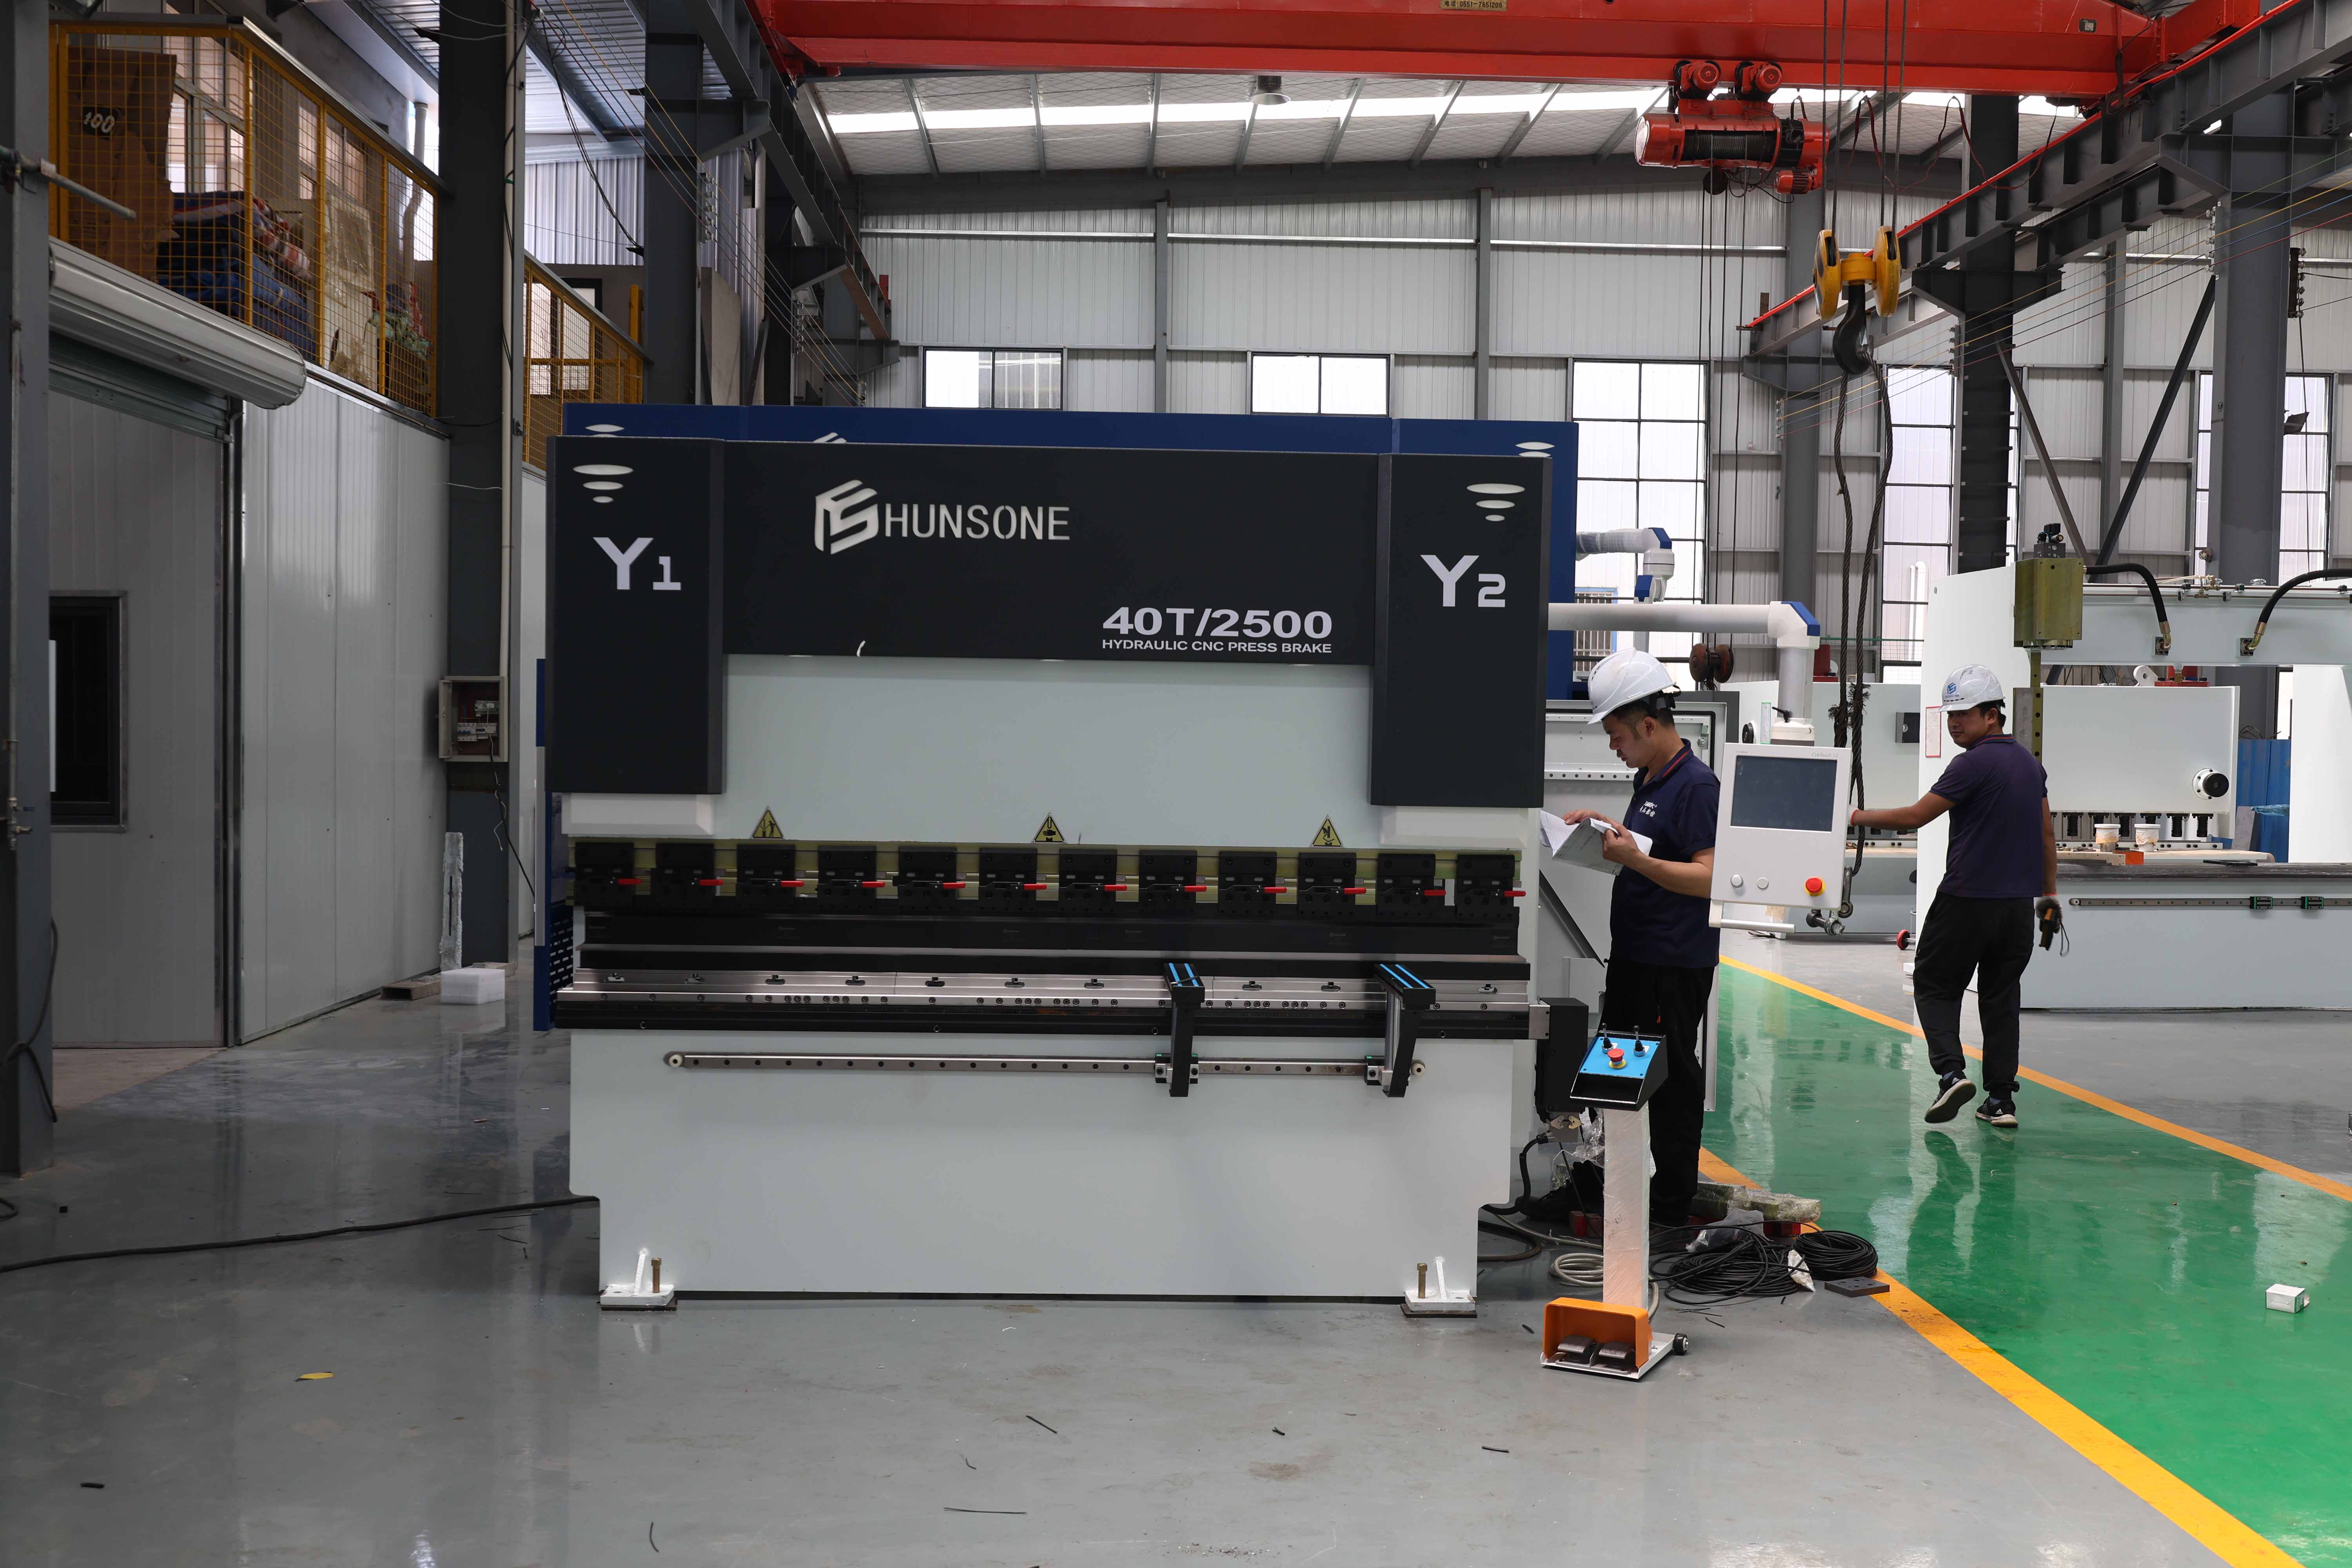
Precision metalworking demands more than just heavy machinery—it calls for a press brake that bends, forms, and shapes metal with absolute control. In this guide, we break down the key features and real-world applications of professional press brake machines, from aerospace brackets to architectural panels. Whether you're upgrading your shop or exploring new fabrication capabilities, understanding what sets a high-performance brake apart can save you time, waste, and costly rework. At HUNSONE, we’ve seen firsthand how the right equipment turns complex bends into repeatable, profit-driving processes. Read on to discover what to look for before your next investment.
Why Frame Rigidity Directly Impacts Bend Consistency
A frame that flexes under load turns every corner into a negotiation. When you lean into a bend, lateral forces travel from the tires up through the wheels and into the chassis. If the frame twists or deflects even a few millimeters, the suspension geometry shifts, altering camber and toe angles mid-corner. That means the grip level you felt at turn-in is not the same grip level you have at the apex, forcing you to constantly adjust steering input instead of holding a smooth arc.
Rigidity matters most in the transition zone between braking and throttle application. On a stiff frame, the load transfer is predictable and linear, so the outside front tire builds up cornering force exactly as you expect. On a flexible frame, that energy gets absorbed and released unevenly, creating a delayed, rubbery response. You end up sawing at the wheel to chase a line that should be stable, and that inconsistency erodes confidence lap after lap.
It is not about making the frame unyielding everywhere. The goal is controlled stiffness in the areas that define suspension pickup points and steering loads. When those hard points stay exactly where the engineers intended, the bend feels repeatable: same entry speed, same steering angle, same exit. Without that repeatability, every corner becomes a guess, and no amount of tire or damper tuning can fully compensate for a chassis that refuses to hold its shape.
Tooling Setup for Short Runs Without Slowing Production
Short-run work only makes money when changeover time stops eating spindle hours. The simplest fix is to standardize tool holders and preset all cutting tools offline. If every mill uses the same pull stud and holder style, operators can swap from one job to the next without touching offsets or re-indicating. A magnetic or tray-based staging cart with pre-measured tools, each tagged with its length and diameter, lets the next setup walk to the machine while the current part is still running.
Fixtures are where most short-run setups die. Lean on quick-change base plates and dedicated subplates per part family. Instead of bolting vises or clamps directly to the table, mount a common receiver plate once and build each job's fixture on its own pallet. Dowel pins and ball-lock fasteners give repeatable location within a few tenths, so you can load a new pallet, tighten four bolts, and be cutting in under ten minutes. Keep all fixture hardware organized by job number so there's no hunting for the right clamp strap.
One thing that gets overlooked is how tool data moves between CAM and the control. Store proven tool assemblies with their stick-out lengths and life counters in the CAM library, not just in the machine. When a short-run job repeats months later, you pull up the exact setup sheet, grab the numbered tooling from the crib, and the machine is ready with stored work offsets. That kills the slow, error-prone process of re-proving every tool on the fly.
Crowning Systems: Keeping Angles True Across the Full Length
When a machine frame stretches beyond three or four meters, even a well-built beam will sag under its own weight and the force of a moving tool head. That sag might measure only a few microns at the center, but at the cutting edge or forming blade, it translates into a measurable angular error—parts come out with a slight taper, or a bend misses its target angle by half a degree. Crowning systems exist precisely to cancel out this deflection. Instead of hoping the structure stays straight, the system intentionally introduces a controlled curve that mirrors the expected sag, so the working surface or tool path remains true from one end to the other.
The compensation can be built into the geometry itself, such as a bed or rail machined with a subtle crown that flattens under load, or it can be dynamic, using a row of hydraulic or mechanical support points that adjust in real time based on sensor feedback. In either case, the goal is the same: keep the angle between the tool and the workpiece constant across the full travel length. On a long press brake, for example, the ram may bend upward in the middle during a full-width bend. A crowning system counters that with a series of wedges or an adjustable lower beam that pushes the die into a slight opposite curve, so every inch of the bend sees the same force and produces the same angle.
Properly set up, a crowning system turns a long machine from a source of constant adjustment into a predictable unit. Operators no longer need to shim the center or over-bend the ends to compensate for deflection. The angle stays true whether the part is at the far left, dead center, or far right of the working envelope. It is one of those details that rarely gets mentioned in product brochures, but for anyone running wide sheet metal, long extrusions, or continuous web processes, it is the difference between scrap and repeatable parts.
Backgauge Positioning Tricks That Reduce Non-Cutting Time
Most press brake operators treat the backgauge as a simple stop, but smart positioning can shave seconds off every bend cycle. Instead of letting the gauge travel from its home position for each part, program the sequence so it moves only the minimum distance between bends. For example, when working with a multi-bend part, keep the backgauge close to the next bend line rather than sending it back to a default position after each stroke. This small change eliminates wasted travel time and lets the machine spend more time forming metal.
Another underused trick is overlapping gauge movements with the ram cycle. On CNC press brakes, you can set the backgauge to reposition while the ram is still descending or retracting. Synchronizing these motions means the gauge is already in place by the time the next bend starts, cutting the non-cutting interval dramatically. It requires fine-tuning the dwell and speed parameters, but once dialed in, the machine feels noticeably faster without any compromise on accuracy.
Finally, consider using multiple backgauge fingers creatively. Instead of a single contact point, position two or four fingers asymmetrically to support flanges of different widths without needing to reprogram between parts. This lets you run a mixed batch with zero gauge setup changes—each cycle simply drops the part against whichever finger is already in the right spot. The result is less idle time, fewer manual adjustments, and a smoother flow from one piece to the next.
Springback Compensation: Planning for Material Memory
Springback isn't a flaw to be fought after the fact; it's a material behavior you can map before the first bend. Every alloy carries a kind of elastic memory, and compensation means working with that memory instead of against it. Rather than relying on generic overbend tables, effective planning starts by quantifying how a specific sheet responds to a given radius, thickness, and grain direction. Small test coupons, bent and measured under production-like conditions, reveal the gap between the tool angle and the final relaxed angle. That gap becomes your baseline, but it rarely stays constant across a long run—tool wear, coil-to-coil variation, and even ambient temperature shift the springback window.
Once the baseline is captured, the next step is to build adjustability into the tooling strategy. Fixed compensation dies work only when the material and process are unusually stable. A more robust approach uses staged tryouts where the punch or wiper geometry is intentionally left with a small range of shim or insert adjustment. This lets the shop fine-tune the overbend without recutting steel. For high-volume or safety-critical parts, in-process angle monitoring tied to a simple correction algorithm can nudge the ram position bend by bend—keeping the final shape inside tolerance even as the incoming material drifts. The key is to treat springback not as a one-time calculation but as a living offset that responds to what the metal actually does, not what the spec sheet promises.
Finally, planning for material memory means documenting the compensation logic so it transfers across shifts and future jobs. Instead of a note that says “overbend 3 degrees,” record the measured springback ratio, the grain orientation tested, and the adjustment range that worked. That turns tribal knowledge into a repeatable starting point for the next part family. Over time, those notes become a practical springback library—saving setup hours and preventing the classic trap of rediscovering the same correction on every new die. The goal is a process that anticipates the metal's return, rather than reacting to it after the first off-spec part hits the bench.
Hydraulic or Electric: Matching Drive Type to Your Workload
Choosing between hydraulic and electric drive systems comes down to the specific demands of your workload, not a simple preference for one technology. Look first at the torque-speed curve and duty cycle. Hydraulics deliver high force at low speeds and handle sudden load spikes with less risk of stalling, which makes them a strong fit for presses, crushers, or lifting applications that cycle hard and often. Electric drives, by contrast, shine when the task needs precise speed regulation, repeatable positioning, or frequent starts and stops without the fluid heating issues that hydraulics can develop.
Another practical angle is how the drive interacts with the rest of your equipment. If you already run a central hydraulic power unit, adding another cylinder or motor is often cheaper and simpler than installing a new servo drive plus cabling and controls. But if your facility lacks hydraulic infrastructure, the cost of hoses, fittings, filtration, and oil disposal can add up fast. Electric actuators are also easier to instrument for data collection, which matters when you need to monitor force, position, and cycle counts in real time. On the other hand, a hydraulic circuit naturally cushions shocks and can hold position under heavy load without power, something an electric brake must be sized to do.
Don't overlook environment and maintenance. Hydraulic fluid leaks, temperature swings, and contamination are ongoing concerns in dusty or washdown areas, while electric drives generally tolerate cleaner conditions but can suffer from overheating if the duty cycle is underestimated. A hybrid approach often works well: use hydraulics for the high-force, short-stroke axis and electric servos for the long-travel or high-precision axes. The right match is not about which technology is newer, but about which one aligns with the load profile, available utilities, and the skill set of your maintenance team.
FAQ
A professional press brake offers closed-loop CNC control, heavier frame construction, and precise ram positioning, allowing it to hold angular accuracy within fractions of a degree across long bends. Standard benders often rely on manual stops and operator feel, which leads to more variation and slower setup.
Look for a rigid frame with minimal deflection under load, a CNC backgauge with multiple axes, automatic crowning to compensate for bed deflection, and high-resolution linear encoders. These elements work together so bend angles stay consistent from the first part to the last.
They use real-time angle measurement systems and adaptive bending algorithms that adjust ram depth based on material springback and thickness variations. This feedback loop reduces the need for test bends and keeps scrap rates low even when sheet properties shift between batches.
Press brakes are central in sheet metal shops serving automotive, aerospace, electrical enclosures, agricultural equipment, and architectural metalwork. Any sector needing brackets, frames, panels, or enclosures with clean, repeatable bends benefits from these machines.
Mild steel, stainless steel, aluminum, and copper are common, but with the right tooling and tonnage it can also form high-strength steels and some alloys. The key is matching the die opening, punch radius, and force to the material's thickness and tensile strength.
Capacity is usually defined by maximum bending length, tonnage, and the largest material thickness at a given die opening. Instead of focusing only on tonnage, consider the required bend length and the inside radius your parts need, because both influence machine deflection and tooling selection.
Regular hydraulic fluid checks, ram and backgauge calibration, and keeping guide rails clean and lubricated prevent most drift and wear. Periodic inspection of tooling for nicks or uneven wear also helps maintain bend quality and reduces the chance of marking workpieces.
It usually sits after cutting and punching operations such as laser or turret punch, and before welding, coating, or assembly. The press brake turns flat blanks into three-dimensional components, so its accuracy directly affects how well downstream assembly fits together.
Conclusion
On a press brake, the frame is more than a structural shell; it is the quiet determinant of every bend. Even a slight flex under load rearranges the angle near the center versus the ends, which is why heavy welded frames and machined reference surfaces matter so much in precision metalworking. Crowning systems build on that stability by compensating for deflection in real time or through hydraulic shimming, keeping angles true across the full working length. The backgauge, often overlooked, has an outsized effect on throughput. Simple improvements like programming multi-step moves, using retract functions to clear tall flanges, and setting approach positions away from the bend line can remove seconds from each cycle. Those seconds accumulate rapidly in high-mix production.
Tooling strategies also shape the balance between speed and accuracy. Ground precision tools with quick-change clamping and segmented punches let a shop move from one part number to the next without excessive setup penalties, while maintaining repeatability for short runs. Material behavior remains the wildcard, so springback compensation has to be planned rather than improvised. Stored angle corrections, bend simulation, and test bends for each new lot prevent the kind of drift that shows up only after inspection. Finally, drive type is not a badge of preference but a workload decision. Hydraulic machines absorb heavy, wide jobs with consistent force, while electric drives offer rapid cycles and precise ram control for lighter, repetitive work. Matching that choice to the mix of materials, thicknesses, and batch sizes keeps a press brake earning its floor space.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/